Engineered Fasteners & Surface Engineering
DUROX provides integrated fastener solutions built for extreme corrosive, cryogenic, and high-pressure operating environments. Browse our product spectrum, international standard coverage, and certified coating formulations below.
Bolts & Studs Series
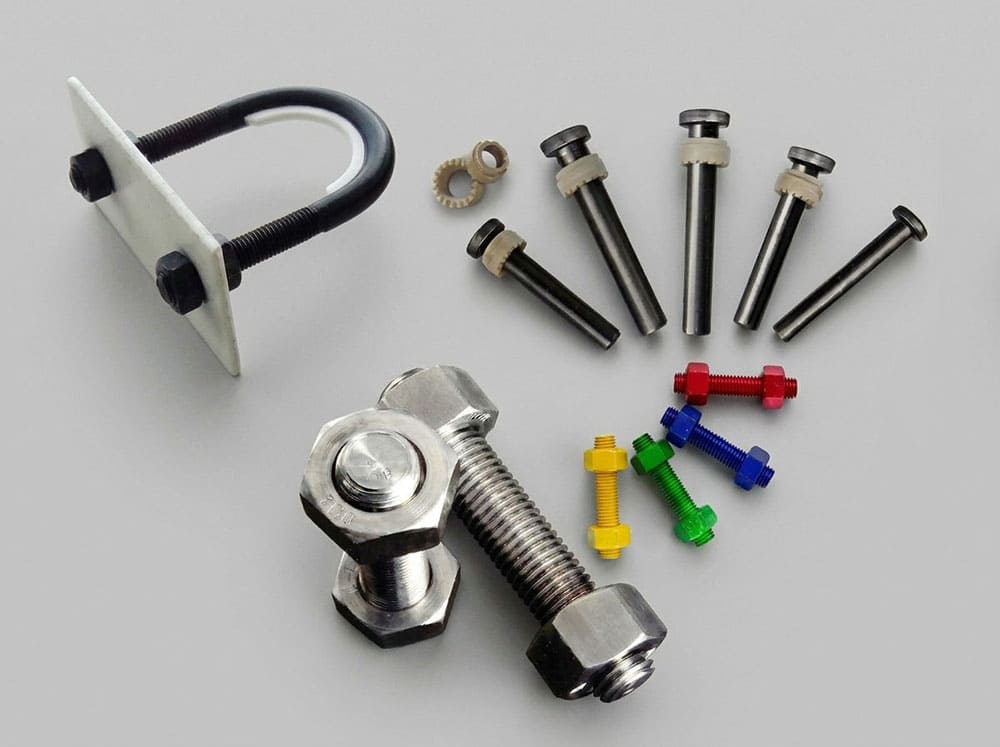
Bolts, Studs & Clamping Sets
- Hex Head Bolts & Screws
- High Strength Heavy Hex Structural Bolts
- Full Thread Stud Bolts (Continuous Thread)
- Double-End Stud Bolts
- Socket Head Cap & Set Screws
- Welded Studs & Foundation Anchor Bolts
- U-Bolt Assemblies, Pipe Clamp Sets & Insulated Clamps
Industrial Nuts Series
Hex, Heavy & Structural Nuts
- Standard Hex Nuts
- Heavy Hex Nuts
- High Strength Structural Steel Nuts
- Self-Locking & Prevailing Torque Lock Nuts
Washer Systems
Plain Flat Washers, Spring Lock Washers, Square Taper Beveled Washers, and Direct Tension Indicators (DTI).
API 20E & Custom Fasteners
Critical Subsea & Custom Machining
API 20E BSL1 / BSL2 / BSL3
Certified Alloy and Carbon Steel Bolting for Use in the Petroleum and Natural Gas Industries. Full metallurgical and manufacturing traceability.
Custom Non-Standard Parts
Custom manufactured components based on engineering drawings, custom thread forms, stepped diameters, and specialty alloys.
High-Performance Material Grades
Comprehensive alloy portfolio certified to ASME, ISO, DIN, GOST, and GB requirements. Engineered for high-temperature, high-pressure, cryogenic, and severe corrosive marine environments.
Carbon & Alloy Steel
Structural & Pressure Fasteners
Designed for high-stress pressure vessels, structural steel frameworks, petrochemical pipelines, and low-temperature service. Heat-treated to ensure precise mechanical properties and controlled hardness for sour-service compliance.
Bolts & Studs Series
ASTM / ISO / GB / GOST Pressure & Structural Bolting
Heavy Hex & Standard Nuts
Matching Hardness & Proof-Load Rated Standards
Stainless Steel
Austenitic & High-Strength Series
Resistant to atmospheric oxidation, acidic media, and chemical process corrosion. Includes stabilized grades (321, 347), high-molybdenum grades (316, 6Mo S31254), and precipitation-hardening high-temp alloys (A453 660).
Stainless Steel Bolts & Studs
ASTM A193 / A320 / F593 / A453 & ISO 3506-1
Stainless Steel Nuts
ASTM A194 / F594 & ISO 3506-2 / GB 3098.15
Duplex Stainless Steel
Duplex & Super Duplex Alloys
Combines high yield strength (twice that of standard austenitic grades) with superior resistance to pitting, crevice corrosion, and chloride stress corrosion cracking (SCC) for subsea and offshore platforms.
Duplex Steel Standards & Grades
Bolts, Studs, Heavy Nuts & Specialty Turned Fasteners
Standard 22% Cr duplex steel offering excellent general corrosion resistance, high fatigue strength, and low thermal expansion compared with austenitic grades.
25% Cr super duplex steel with additions of tungsten and copper (Zeron® 100 type). Designed for severe marine and acidic sour gas subsea applications.
Every batch of Duplex & Super Duplex fasteners undergoes 100% PMI verification, ASTM E562 ferrite content measurement (35% - 55%), ASTM A923 Method C ferric chloride pitting test, and Charpy V-notch impact testing at low design temperatures.
Nickel-Base Alloys
Nickel Specialty Alloys
Engineered for extreme service conditions where conventional steels fail: critical sour gas wells (H₂S/CO₂), downhole drilling tools, aerospace turbines, and chemical reactors.
Nickel Alloy Standards & Grades
Precision Machined Bolts, Studs & Heavy Nuts
Precipitation hardenable nickel-chromium alloy with high creep-rupture strength up to 700°C and outstanding resistance to post-weld cracking.
High resistance to pitting and crevice corrosion across a broad spectrum of severely corrosive environments from cryogenic to 982°C.
Solid-solution binary alloy showing exceptional resistance to rapidly flowing seawater, hydrofluoric acid, sulfuric acid, and alkalies.
Nickel-chromium-iron-molybdenum superalloy exhibiting outstanding high-temperature oxidation resistance, formability, and stress rupture strength.
Copper & Alloys
Copper & Bronze Fasteners
Provides superior biofouling resistance, non-magnetic properties, and spark-free safety characteristics for marine seawater intake systems, valves, and electrical switchgear assemblies.
Copper Alloy Standards & Grades
Aluminum Bronze & High-Conductivity Brass Fasteners
Heavy-duty nickel-aluminum bronze offering excellent wear resistance, high shock load capacity, and complete immunity to seawater cavitation erosion.
High electrical and thermal conductivity, excellent cold-heading ductility, and smooth thread engagement for instrumentation and busbar connections.
Full Material Traceability & QA Certification
All fasteners are marked with traceable heat lot codes and supplied with 3.1 or 3.2 inspection certificates covering raw material chemical composition, tensile, yield, elongation, impact, and coating thickness test reports.
Request MTR / Spec Sheet
Fill in the form and our team will get back to you shortly.
Request MTR / Spec Sheet
High Quality Sheradizing Coating
A thermal diffusion zinc-iron alloy surface protection process engineered for demanding marine, offshore, chemical, and structural steel applications.
Thermal Diffusion Metallurgy & Protection
Sheradizing is a thermal diffusion surface protection process where fine zinc powder is vaporized and diffused into the steel substrate, creating a hard, sacrificial zinc-iron (Zn-Fe) alloy intermetallic layer.
Serving as an impermeable metallurgical barrier, it completely isolates the steel core from hostile atmospheric elements. In humid, aggressive offshore, or subsea environments, the uniform alloy matrix behaves as an active yet highly stable galvanic anode, delivering exceptional electrochemical cathodic protection against rust and pitting.
Operating at controlled low diffusion temperatures, the process eliminates the hazard of hydrogen embrittlement, fully preserves the original mechanical tensile properties of high-strength fasteners, and runs under an environmentally benign, zero-emission process envelope.
Target Industrial Applications
Zero Hydrogen Embrittlement
Acid-free thermal diffusion process guarantees no hydrogen absorption, making it safe for 10.9, 12.9 & high-strength alloy fasteners.
Precise Thread Uniformity
Micron-level even dispersion (15-85 μm) across root threads, complex geometries, and recesses with zero bead clogging or retapping needed.
Exceptional Hardness & Wear
Zn-Fe intermetallic alloy exhibits high surface micro-hardness (up to 400+ HV), offering superior abrasion resistance and anti-galling.
5,000 hrs Salt Spray (NSS)
Delivers up to 5,000+ hours neutral salt spray resistance at an economical cost basis, providing superior lifecycle ROI.
Coating Systems Comparison Matrix
Detailed performance comparison of Sheradizing against Hot-Dip Galvanizing (HDG), Zinc Plating, Zinc-Nickel, and Fluoropolymer systems.
| Performance Parameter | Zn-Plating | Zinc + Xylan® | Zn-Ni Plating | Zn-Ni + Xylan® | Xylar® 2 + Xylan® | HDG (Hot-Dip) | Mech. Zinc | Sheradizing |
|---|---|---|---|---|---|---|---|---|
| Coating Thickness (μm) | 8 ~ 13 | 23 ~ 38 | 8 ~ 13 | 23 ~ 38 | 35 ~ 55 | 45 ~ 120 | 25 ~ 110 | 15 ~ 85 |
| Corrosion Resisting Life | Short | Comparatively Long | Long | Comparatively Long | Comparatively Long | Long | Normal | Long |
| Hydrogen Embrittlement Risk | Yes | No | Yes | No | No | Less | No | No |
| Effect on Component Strength | No | No | No | No | No | Yes (High Temp) | Yes | No |
| Effect on Component Fitness | Minimal | Minimal | Minimal | Minimal | Minimal | Large (High Buildup) | Minimal | Minimal |
| Level of Adhesion | Good | Good | Good | Good | Good | Good | Poor | Excellent / Alloyed |
| Coating Uniformity | Good | Preferable | Good | Preferable | Preferable | Very Poor | Normal | Excellent |
| Zinc Utilization Rate | High | High | High | High | -- | Lower | High | High (Eco) |
| Production Efficiency | High | High | High | High | High | High | High | High |
| U-Bolt & Complex Fit Suitability | Good | Preferable | Preferable | Preferable | Preferable | Poor | Poor | Excellent |
| Neutral Salt Spray Test (Hours) | 96 hrs | 2,500 hrs | 5,000 hrs | 5,000 hrs | 5,000 hrs | 2,500 hrs | 2,500 hrs | 5,000 hrs |
| Relative Cost / Price Level | Economical | Moderate | Premium | High+ | Highest++ | Economical | Economical | Economical / Cost-Effective |
Need Specification Guidance for Sheradized Fasteners?
DUROX engineers can assist with alloy compatibility, standard conformance (EN, ISO, ASME, GOST), and coating thickness selection for your offshore or critical infrastructure projects.
Consult Our Specialists
High Quality Xylan® Coating Solutions
Engineered fluoropolymer barrier coatings developed since 2002 for extreme subsea, petrochemical, and heavy marine environments.
High-Performance Alternative to Costly Exotic Superalloys
Since 2002, DUROX INDUSTRIAL has engineered premium anti-corrosion coated stud bolts, hex nuts, and threaded components widely deployed across upstream offshore drilling, subsea flowlines, and downstream refinery facilities.
Leveraging genuine Whitford® Xylan® matrix technology, our coated carbon and alloy steel fasteners provide exceptional dry-film lubrication, galling resistance, and severe barrier protection. This delivers a vastly more cost-effective, readily available alternative to solid stainless steel, nickel alloys (Inconel 625/718), and titanium hardware without sacrificing operational integrity.
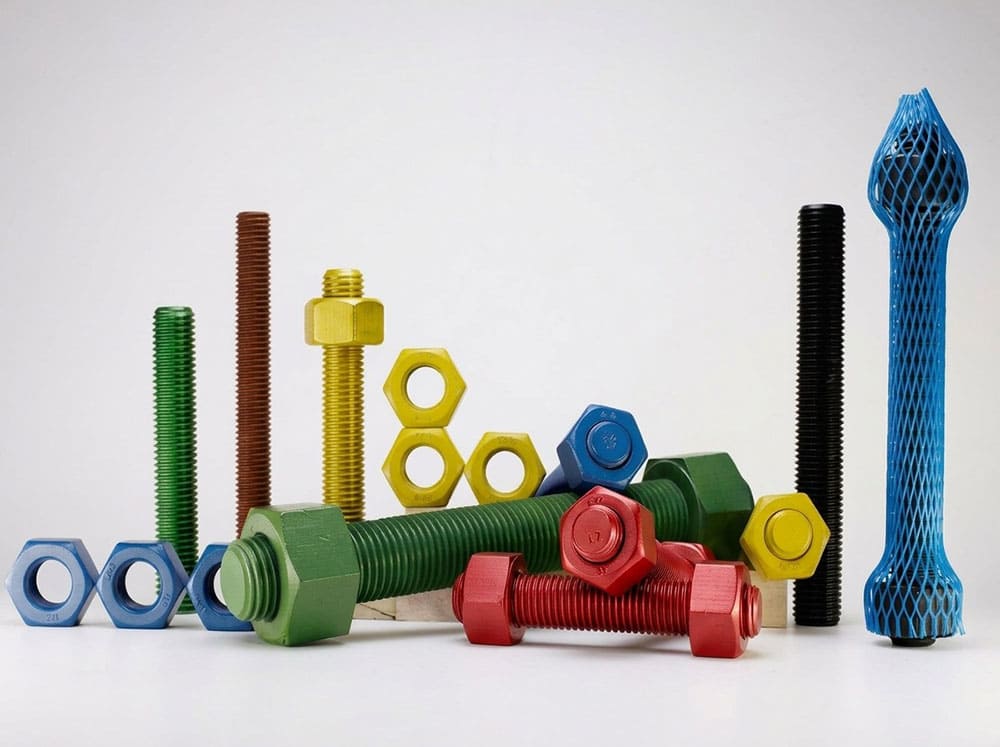
Xylan® Coating Key Advantages
Engineered multi-layer matrix providing chemical inertness, low breakout torque, and structural reliability in extreme exposure.
Friction Reduction
Drastically lowers thread coefficient of friction to predictable levels (0.055-0.080), eliminating bolt chatter and irregular clamping loads.
Dry Film / Self-Lubricating
Eliminates the requirement for wet thread grease. Clean dry-film matrix ensures smooth, repeatable make-up and precise bolt tensioning.
Wear & Galling Resistance
Prevents thread galling, seizure, and thread stripping during high-torque assembly and rapid pneumatic torquing operations.
Atmospheric Anti-Corrosion
Exceptional salt-spray resistance over 2,000 to 5,000 hours without red rust, protecting structural joints against coastal salt-fog.
Chemical & Acid Resistance
Resistant to harsh acids, alkalies, H₂S, hydrocarbons, CO₂, and caustic cleaning solvents common in processing facilities.
Thermal Stability
Maintains film integrity across cyclic thermal shocks from arctic/cryogenic environments to high-temperature piping systems.
Non-Stick & Easy Breakout
Hydrophobic, oleophobic surface repels debris, mud, and bitumen, allowing fast maintenance breakout without hot-bolting or cutting torches.
Eco-Friendly Formulation
Manufactured with low-VOC, heavy-metal-free, REACH & RoHS compliant formulations, ensuring environmental safety throughout product lifecycle.
Advanced Application Equipment
Our temperature- and humidity-controlled facility utilizes automated robotic arms and calibrated precision coating machinery to guarantee uniform dry film thickness on complex fastener threads.
High-atomization precision air guns providing micro-droplet consistency across thread profiles.
Real-time rheology and efflux viscosity tracking for strict coating batch formulation control.
Continuous ambient temperature and dew point sensors preventing condensation defects.
Full-containment environmental spray booths with multi-stage HEPA particulate filtration.
Uniform hot-air circulation furnaces maintaining ±2°C thermal distribution across all batches.
Continuous multi-zone energy-efficient curing tunnels ensuring complete polymer crosslinking.
Rigorous Inspection & Laboratory Tests
Every batch undergoes certified internal laboratory validation to verify mechanical adhesion, thread gauge compliance, chemical resistance, and salt spray performance.
100% Go/No-Go thread pitch gauge inspection ensuring Class 2A/2B and 6g/6H tolerance engagement.
Spot exposure resistance validation using 5% Sulfuric Acid (H₂SO₄), 5% Acetic Acid (CH₃COOH), and 5% Sodium Bicarbonate (NaHCO₃).
ASTM D5402 MEK rub validation to ensure 100% molecular cross-linking and full chemical polymerization.
ASTM D3359 cross-hatch adhesion (Class 5B), magnetic/eddy-current Dry Film Thickness (25-45 μm), and cyclic neutral salt fog testing up to 5,000 hrs.
Base + Topcoat Engineering Architecture
As a certified Whitford OAC facility, DUROX combines specialized pre-treatments, sacrificial base layers, and authentic Whitford® Xylan® 1000/1400 topcoats to deliver customized barrier performance.
Sacrificial Underlayers
- Zinc Electroplating (ASTM B633)
- Zinc Phosphate / Manganese Phosphate
- Thermal Sherardizing (Zinc Infusion)
- Zinc-Nickel Alloy Plating (12-15% Ni)
- Whitford® Xylar® 2 Cermet Primer
Whitford® Xylan® Matrix
- Xylan® 1424 Series (Fastener Standard)
- Xylan® 1014 (High-Wear Resin Bonded)
- Xylan® 1070 (Low-Friction Barrier)
- Xylan® 1052 (High Pressure Lubrication)
- PTFE / Ceramic / FBE Formulations
Zinc + Xylan® 1424 System
Guaranteed over 2,000+ hours ASTM B117 salt fog endurance without red rust. Zinc-Nickel + Xylan® systems exceed 5,000+ hours for subsea splash zone compliance.
Color-Coded Xylan® Coated Fasteners
Custom engineered colors for quick subsea identification, safety zoning, and operational line classification.
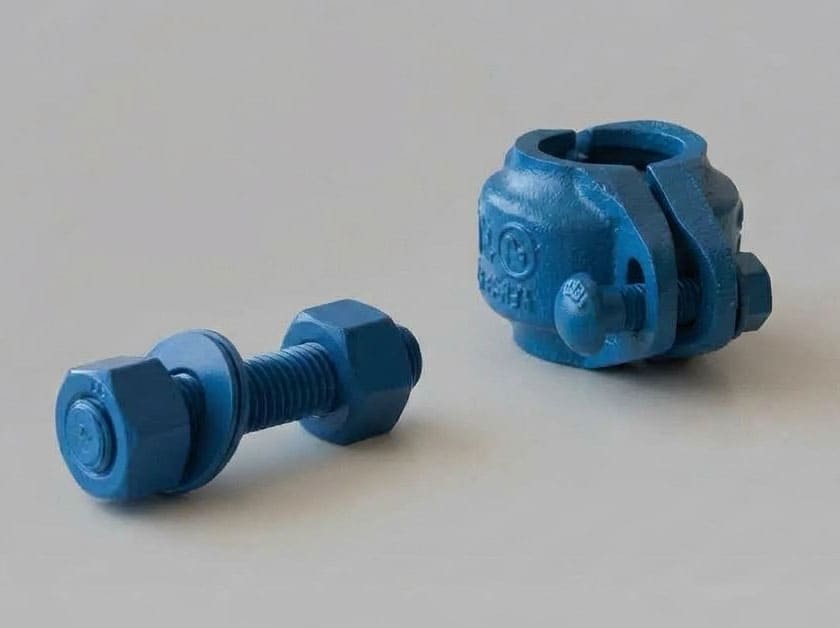 Marine Blue (1424)
Subsea & Flange Stud Bolts
ASTM A193 B7/B7M & A320 L7/L7M full-thread stud bolts with heavy hex nuts for subsea manifolds and Christmas trees.
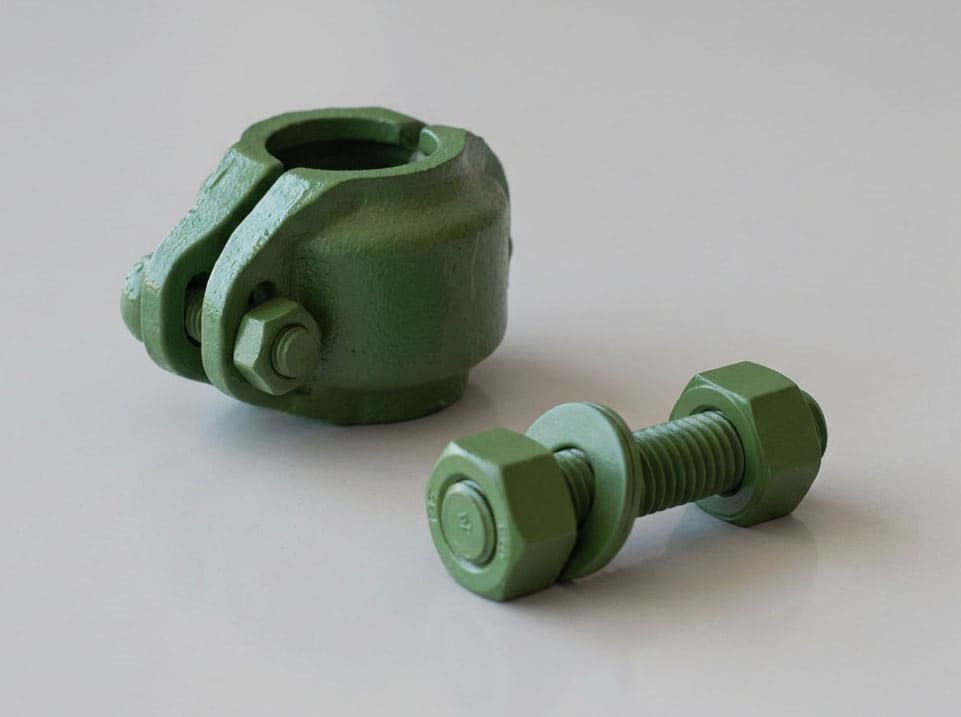 Forest Green (1070)
Chemical & Acid Valve Hardware
High-lubricity fluoropolymer coating for petrochemical pipeline valves, high-pressure pumps, and acid distillation columns.
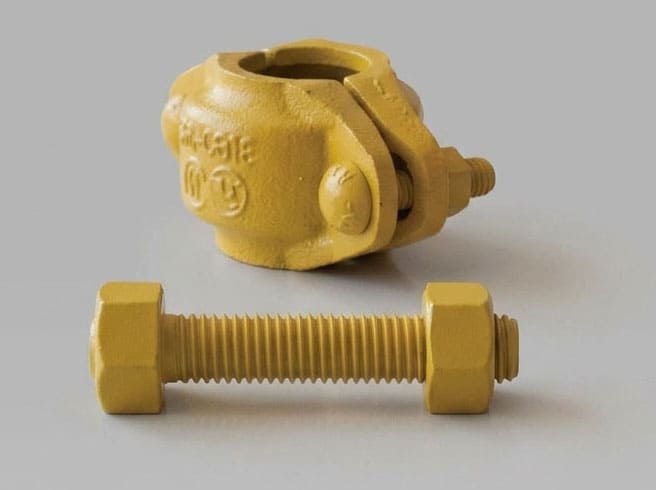 Hi-Vis Yellow (1014)
Offshore ROV-Visible Stud Sets
High-visibility yellow topcoat engineered for deepwater subsea ROV inspection cameras and splash-zone structural clamps.
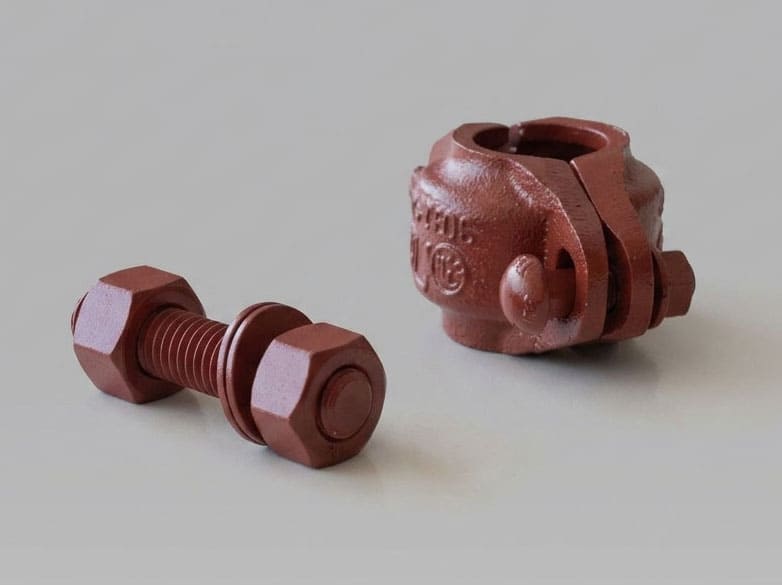 Signal Red (1424)
Fire Line & Emergency Systems
Color-coded high tensile fasteners dedicated to offshore deluge piping, safety isolation valves, and emergency ESD valves.
Require Specific Coating Thickness or Custom Color Formulations?
Our metallurgists and coating engineers offer complete technical validation, torque-tension curves, and third-party witness inspection (BV, DNV, Lloyd's) for your project specifications.
Request Coating Spec Sheet
Fill in your details and we'll send the specification sheet directly to you.
DUROX INDUSTRIAL